Direct Engagement
The short, sturdy body allows the tool to engage the material directly without wandering.
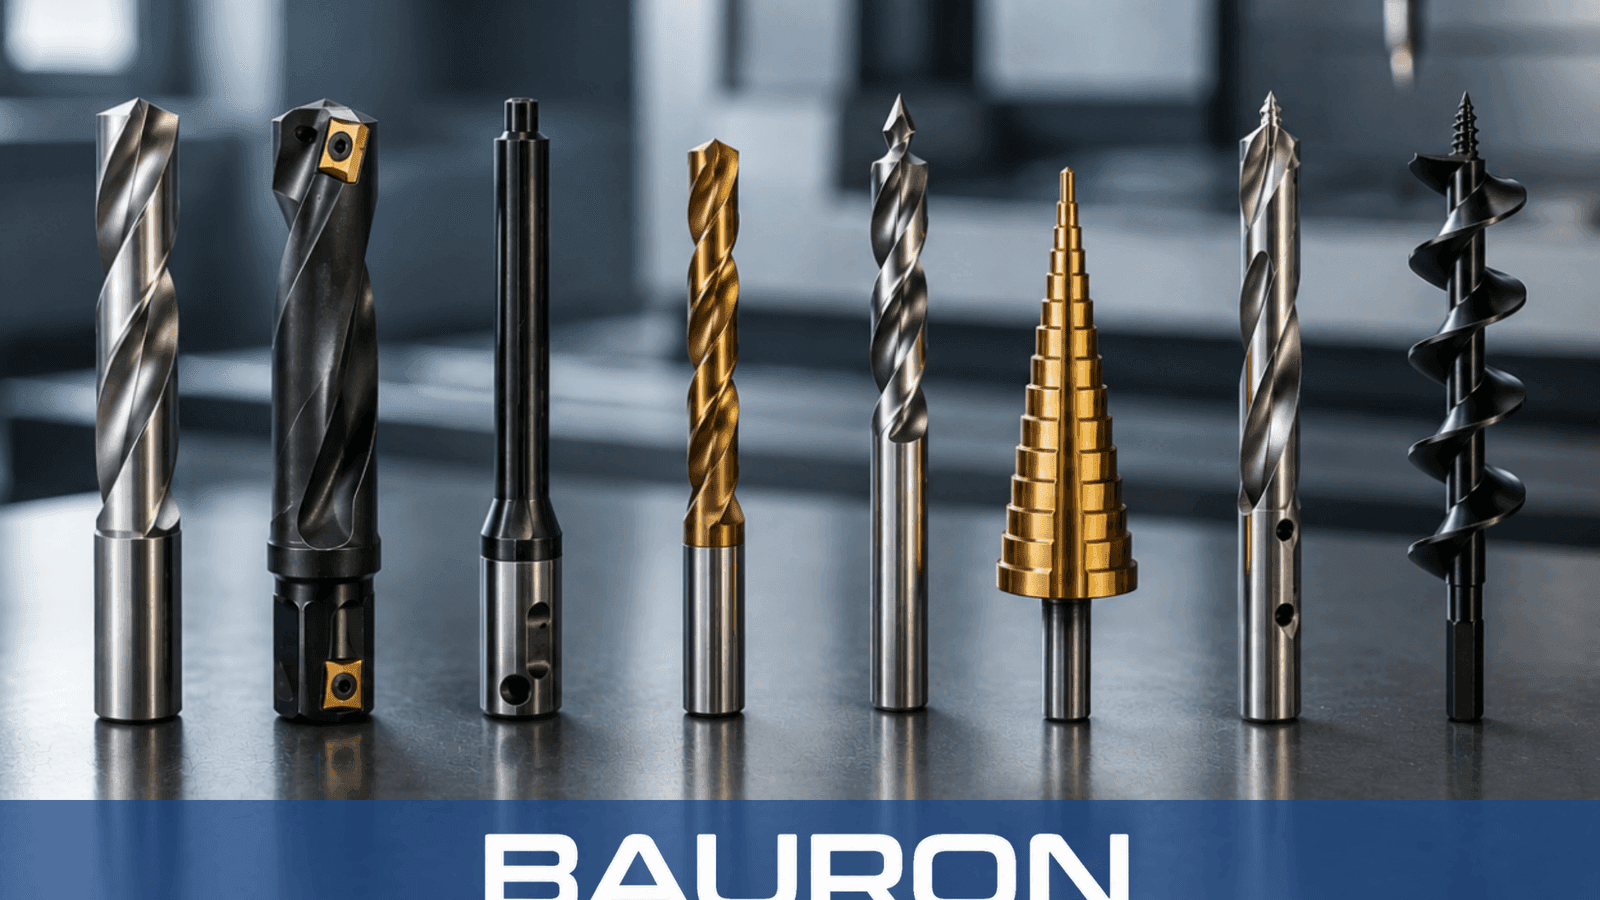
Screw machine length drill bits, often referred to as "stub drills," are specialized cutting tools engineered for maximum rigidity. Originally designed for automated screw machines, their short flute and overall length reduce the leverage forces that cause standard drills to bend or snap during heavy feeds.
The short, sturdy body allows the tool to engage the material directly without wandering.
A typical 135-degree split point bites into the metal immediately, eliminating the need for a center punch or spotting drill.
The reduced flute length provides core strength that limits vibration during the cut.
Reduced deflection helps the drill produce round, accurate holes.
The short profile resists breakage under normal straight-line drilling forces.
The rigid body and split-point geometry can eliminate a separate center-drilling operation.
Thick web construction supports faster feeds than standard-length bits.
The short profile suits right-angle drills and confined mechanical bays.
A complete screw machine drill bit set provides fractional or metric sizes for immediate tool changes.
| Specification | Range / Details |
|---|---|
| Diameter Range | 1/64" to 1" (Standard, Metric, Wire, and Letter sizes) |
| Flute Length | Significantly shorter than Jobber length (approx. 4x to 5x diameter) |
| Point Angle | Typically 135° Split Point for self-centering |
| Shank Type | Straight Cylindrical |
| Tolerance | Precision ground for high-speed CNC applications |
| Format | Individual bits or a complete screw machine drill bit set |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS (High-Speed Steel) | Mild steel, aluminum, and general machining. | Economical and resistant to impact and shock loads. |
| Cobalt (HSS-Co) | Hardened steel, stainless steel, and titanium. | Heat resistance supports aggressive feed rates in tough alloys. |
| TiN / TiAlN Coating | Continuous CNC production environments. | Reduces friction and wear to retain the cutting edge over repeated cycles. |
HSS provides impact resistance and economy for general machining, cobalt adds heat resistance in hard alloys, and TiN or TiAlN coatings reduce friction and wear in repeated CNC cycles.
The original intended machine, used for high-volume automated part turning and hole boring.
Mount the bits in turrets to drill into the center of rotating workpieces with minimal deflection.
Give mechanics and sheet metal workers a short, rigid bit for confined spaces.
Used in CNC lathes and automatic screw machines to drill holes rapidly in continuous production cycles.
Bores clearance and tapped holes where standard jobber drills are too long to fit.
Cuts stainless steel and titanium where tool rigidity is critical to prevent snapping.
Drills round holes in thin metals without catching or distorting the material.
Jobber length bits are longer, all-purpose drills. Screw machine length drill bits are much shorter, which makes them more rigid and limits bending, vibration, and breakage in hard materials.
Typically no. Their rigid bodies and common 135-degree split points resist walking, allowing them to drill directly into the workpiece without a pilot or center hole.
A set provides an organized index of fractional, wire, letter, or metric sizes. It reduces downtime by keeping a rigid bit available for a range of hole dimensions.
Yes. Their short length is useful in tight engine bays and makes them harder to snap accidentally than standard jobber drills.
Cobalt is better suited to stainless steel, cast iron, titanium, and other hard materials because it retains its edge under high heat. Standard HSS is more economical for softer materials such as aluminum or wood.
Bauron provides design and engineering support for application-specific tooling requirements. Share the geometry, material, coating needs, and machining challenge for technical review.
Talk to Engineering